

 Deutsch
 Français
 Español
The use of MIM technology has experienced exponential growth over the last decades, establishing itself as the most important technology in the manufacturing processes of metal parts. However, it is possible to find in FDM and Binder Jetting complements to this technology, so they should not be seen only as competitive processes.
MIM (Metal Injection Moulding)
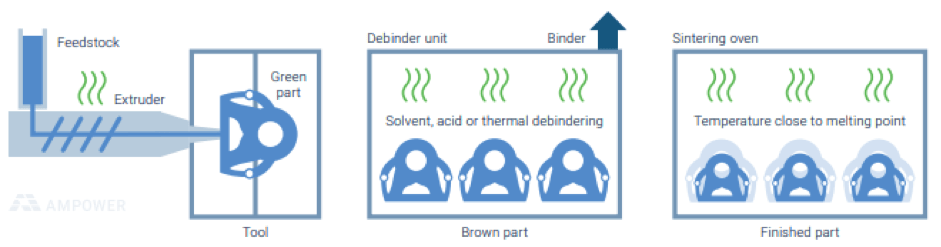
MIM (Metal Injection Moulding) technology is a metal parts manufacturing technology that combines powder metallurgy with plastic injection molding technology. The raw material used is a mixture of metal powder and polymers called feedstock. This material is fed into a mold with the desired geometry by means of an injection machine similar to the one used in the plastic injection molding process. This results in the so-called green part, which is subjected to a chemical-thermal process called desbanderization, the purpose of which is to extract the binder from the part, thus obtaining the brown part. The part is then subjected to the sintering process, so that the particles are joined together to form a high-density metal part with tight dimensional tolerances. MIM technology is suitable for manufacturing parts of complex geometry, small to medium size, and a wide variety of materials are available, such as stainless steels, low alloy steels, soft magnetic, tool steel, ceramics, etc.
FDM Printing
FDM (Fused Deposition Modeling) printing technology, also known as ME (Material Extrusion) or FFF (Fused Filament Fabrication), is the process by which parts are manufactured layer by layer by depositing extruded material (metal powder + polymers) through a nozzle similar to those used in plastic filament printers. This technology can use filament, pellets or rods as raw material and, once the green part is printed, debanding and sintering processes are needed, as in MIM technology, to obtain the final metal part.

Binder Jetting
The manufacturing process of the Binder Jetting technology is based on the deposition of a layer of metal powder on a printing platform and the agglomeration by deposition of polymeric material through a nozzle. Subsequently, polymer curing processes are necessary in each printed layer and, once the printing is finished, the so-called de-powdering process to remove the remaining powder and obtain green parts. Finally, debanding and sintering processes are needed to obtain the metal parts. The debinding process in parts printed by Binder Jetting is less critical than usual, because the amount of binder deposited at the layer junction is minimal. This results in easy removal of the binder from the green part, but at the same time makes the printed green parts fragile and difficult to handle.

Characteristics compared between Binder Jetting, FDM and MIM
Although in many articles you can find comparative graphs of technologies where we see overlap between MIM technology and some printing technology, especially Binder Jetting, the reality is that today Additive Manufacturing and MIM are not competitive technologies but complementary. Some fundamental differences between the two technologies are defined below.

Manufacturing Speed
Although part developments are much faster in Additive Manufacturing compared to MIM, mainly due to mold manufacturing, post-mold part production becomes faster in MIM technology compared to printing technologies.

Differences in porosity and microstructure
Large porosity associated with printing defects may appear, especially in parts manufactured by FDM. This can lead to lower metal part densities than those obtained by MIM. In addition, the nature of the metal powder used in manufacturing can generate incorrect microstructures that require subsequent heat treatments to improve it.

Portfolio of materials
MIM technology is much more versatile in terms of the materials available for manufacturing metal parts. Keep in mind that Additive Manufacturing technologies are in the midst of development and their material portfolio is likely to increase as the technology matures. As of today, the portfolio of materials available in printing technologies is limited to stainless steels, some tool steel and few other materials.

Surface Finish
Increased roughness in Additive Manufacturing techniques. Necessary secondary finishing improvement operations to compete with MIM. In Ecrimesa Group we guarantee sintered roughness between 0.8 and 1.6 Ra.

Design
Possibility of manufacturing more complex parts (hollow parts, bionic geometries, counter-flanges, etc.) and larger parts in Additive Manufacturing technologies.

MIM and Additive Manufacturing technologies working in different market sectors
Although Additive Manufacturing technology is constantly developing and there may be variations, it seems that this manufacturing technology is positioning itself primarily in the medical, industrial and aeronautical sectors.

Mechanical properties
The results of a comparative study of mechanical properties (tensile test) of sintered 17-4PH specimens are shown. Tensile specimens are manufactured according to ISO 2740 Sintered metal materials (excluding hardmetal) according to the different technologies and printers described in the following table.
| Technology / Printer | Density (g/cc) | Hardness (HV10) | Ultimate tensile strength Rm (MPa) | Yield strength Rp0,2 (MPa) | Elongation A (%) |
| MIM | 7,63 | 296 | 951 | 839 | 5,1 |
| FDM Conventional 3D printer | 7,53 | 271 | 811 | 749 | 6,4 |
| FDM Desktop Metal | 7,57 | 274 | 852 | 806 | 3,2 |
| Binder Jetting | 7,57 | 260 | 870 | 777 | 6,7 |
| ISO 22068 MIM-174PH Sinter | 7,50 | 280 | 800 | 650 | 3 |
All the mechanical properties obtained are within the ISO 22068 “Sintered metal injection molded materials specifications” for sintered 17-4PH steel, with the MIM technology showing the best mechanical properties.
Click here to the link:


 by